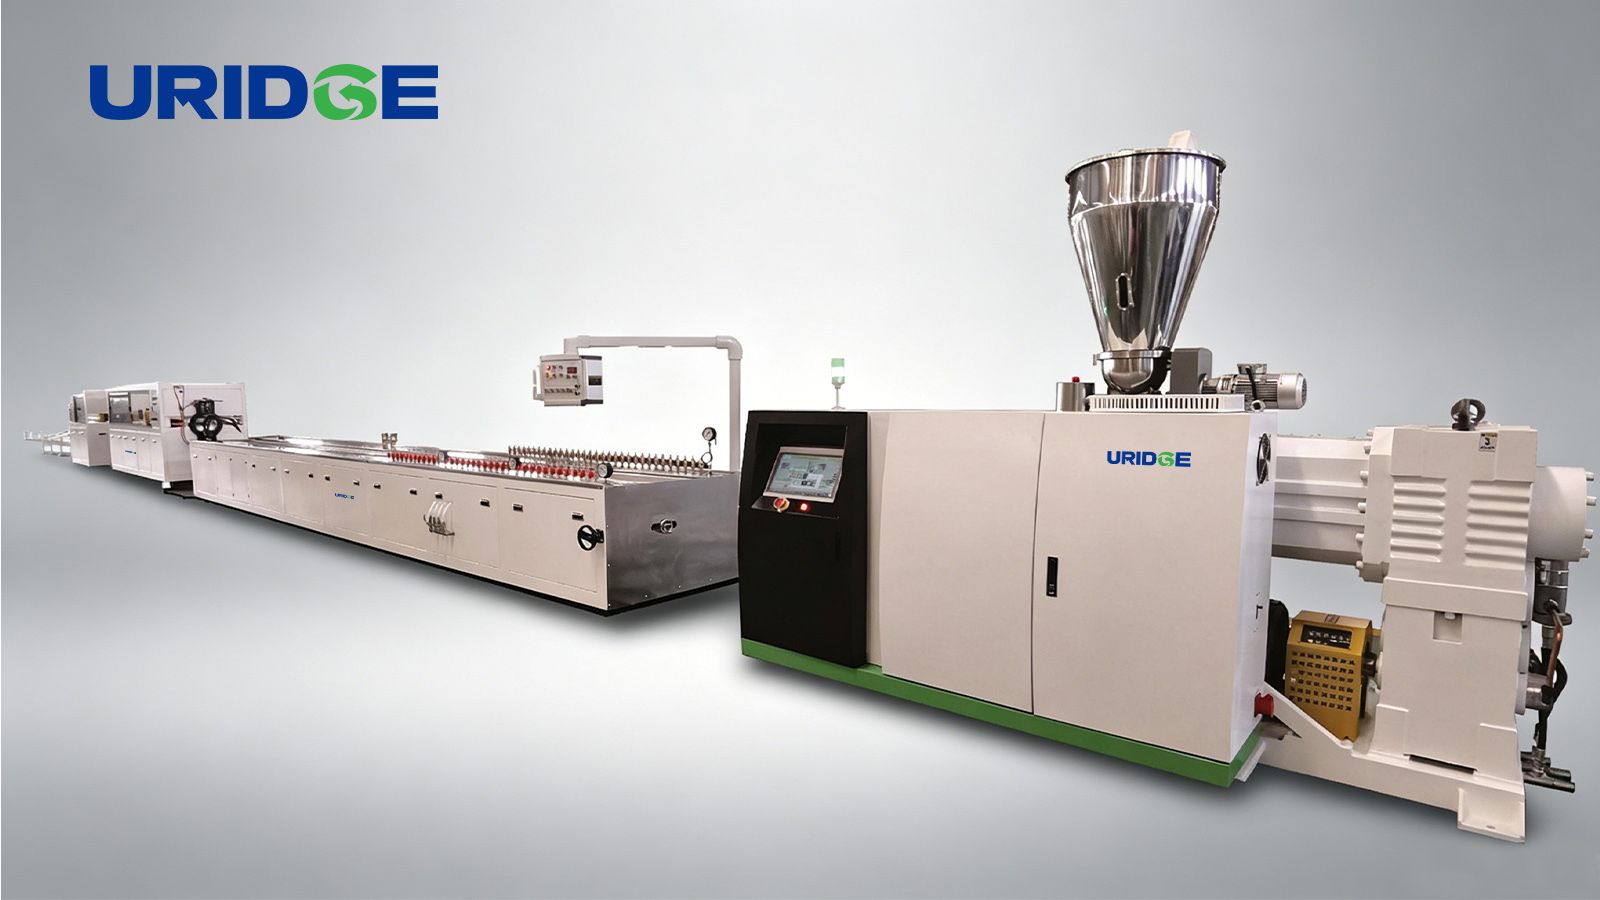
Plastic Profile Extrusion Line
Multi-Material Plastic Profile Extrusion Line
URIDGE builds plastic profile extrusion lines for PVC, WPC, PE, PP and ABS, with customized dies, single or twin-screw extruders and co-extrusion options.
- Turnkey design & installation
- ISO9001 / CE certified
- 24/7 global after-sales support
Product Overview
The URIDGE Multi-Material Plastic Profile Extrusion Line is designed for the production of rigid and flexible profiles in PVC, WPC, PE, PP, ABS and other suitable thermoplastics.
The line can be configured for a wide range of profile applications, including window and door profiles, electrical cable trunking, skirting boards, decorative profiles, wall panels, furniture profiles, WPC profiles, hollow sections, low-foamed profiles and flexible sealing strips.
The extrusion system, screw configuration, die, calibration system and downstream equipment are selected according to the raw material, profile cross-section and production requirements.
For different materials, different extrusion technologies are used. PVC and WPC profiles are commonly produced with twin-screw extruders, while PE, PP and ABS profile applications typically use single-screw extruders.
Profile Applications
The line can be configured for applications across the construction, decoration, electrical, furniture, appliance and transportation industries.
Typical products include:
- Window frames
- Door frames
- Window sills
- Skirting boards
- Corner profiles
- Wall panels
- Electrical cable trunking
- Furniture edging
- Decorative strips
- Cabinet profiles
- Flexible sealing strips
- Automotive interior and exterior trim profiles
Flexible PVC is particularly suitable for sealing and decorative profiles used in automotive and window-and-door applications.
Materials and Extruder Selection
Different polymers require different extrusion configurations.
PVC and WPC applications typically use twin-screw extrusion systems for stable processing of powder-based or compounded materials.
PE, PP and ABS profiles generally use single-screw extruders.
The final extruder specification is selected according to the material formulation, profile dimensions, cross-sectional complexity and required production capacity.
Production Process
A typical profile extrusion line follows this process flow:
Raw Material → Feeding → Single-Screw or Twin-Screw Extrusion → Profile Die → Calibration and Cooling → Haul-Off → Cutting → Collection.
Feeding and Extrusion
The feeding system transfers prepared raw material to the extruder. Depending on the polymer, the line can use either a single-screw or twin-screw extruder to plasticize and homogenize the material before it enters the profile die.
Profile Die
The profile die determines the cross-sectional geometry of the final product. URIDGE designs the die according to the customer’s profile drawing, material and product structure. Die complexity and configuration therefore depend strongly on the shape and functional requirements of the profile.
Calibration, Haul-Off and Cutting
After leaving the die, the profile passes through the calibration and cooling system to stabilize its dimensions and shape. The haul-off unit maintains a controlled pulling speed, while the cutting system cuts the finished profile to the required length before collection.
Extrusion Control and Automation
Screw and Barrel Temperature Control
For applications requiring precise melt-temperature control, the extrusion system can incorporate internal screw oil cooling together with copper-tube cooling around the front section of the barrel. These cooling arrangements help control thermal conditions in critical extrusion zones and support more stable profile formation.
Pressure Closed-Loop Control
A pressure closed-loop control strategy can be used to improve extrusion stability. By monitoring and controlling melt pressure, the system helps maintain more stable material flow through the die, supporting consistent profile formation and dimensional stability.
Automation and Control
The production line can be equipped with Siemens PLC control and an HMI touchscreen interface. PID-based adaptive temperature control is used for extrusion temperature management. Optional automatic weighing and feeding systems can be configured according to production requirements.
The control system can also include:
- Pressure closed-loop control
- Overcurrent protection
- Overvoltage protection
- Recipe storage
- PLC remote communication module
Functional Co-Extrusion
Co-extrusion can be configured when a profile requires an additional functional material. For example, a small flexible material section can be co-extruded onto a rigid profile to provide sealing or other functional properties.
The co-extrusion arrangement is designed according to the profile structure, material combination and customer drawing.
Customized Profile Dies
Profile tooling is developed according to the customer’s final product drawing. Die pricing and configuration depend on the profile cross-section, dimensions, material, structural complexity and functional requirements. Customers are therefore encouraged to provide a profile drawing or sample when requesting a machine and tooling quotation.
Flexible Line Configuration
URIDGE profile extrusion lines are configured according to the customer’s raw material and final profile. Configurable items can include:
- Extruder type
- Screw configuration
- Profile die
- Feeding system
- Electrical component brands
- Motor brands
- Automation level
- Downstream equipment
The main selection factors are the polymer, profile shape, cross-sectional complexity, required output, plant conditions and local electrical standard.
Factory Testing
The production line is tested before shipment. Customers can also provide their own raw material for trial production so that the machine, die and processing conditions can be evaluated before delivery.
Installation and Technical Support
URIDGE provides installation, commissioning and operator training for profile extrusion lines. Remote technical support and spare-parts support are also available.
- Typical warranty period: 1 year
- Typical production lead time: approximately 2 months
- Typical installation period: approximately 1 week
Before installation, customers should prepare suitable floor conditions and ensure that the required electricity, water and compressed-air connections are available.
Project Experience
URIDGE has supplied profile extrusion equipment for customers in markets including Iraq, Turkey, Cambodia, Hungary, Malaysia and Indonesia. Applications have included window and door profiles, electrical trunking, decorative panels and related profile products.
Frequently Asked Questions
What materials can the profile extrusion line process?
The line can be configured for PVC, WPC, PE, PP and ABS profile production. Extruder type, screw design, tooling and downstream equipment are selected according to the material and final profile.
Should I use a single-screw or twin-screw extruder?
PVC and WPC profiles typically use twin-screw extrusion systems, while PE, PP and ABS applications generally use single-screw extruders. Final selection depends on the raw material formulation and product requirements.
Can URIDGE manufacture the profile die?
Yes. The profile die can be designed according to the customer’s product drawing, material and cross-sectional structure.
Can the line produce flexible PVC profiles?
Yes. The line can be configured for flexible PVC products such as sealing strips and decorative profiles used in automotive and window-and-door applications.
Does the line support co-extrusion?
Yes. Co-extrusion can be configured when the profile requires an additional functional material, such as a flexible sealing section on a rigid profile.
Can I send my own material for testing?
Yes. Customers can provide their own material for trial production before shipment.
Send Us Your Profile Drawing
To configure a suitable profile extrusion line, please send us:
- Raw material
- Final profile drawing or sample
- Profile dimensions
- Required production capacity
- Single-material or co-extrusion requirement
- Local voltage and frequency
- Available factory space
URIDGE will recommend the extruder, tooling and downstream configuration according to your actual profile. You can request a quote or contact us directly to start the configuration.
Technical Specifications
Detailed parameters (capacity, screw diameter, installed power, dimensions, voltage) are tailored to your material and output requirement.
Request Spec Sheet Get a Quote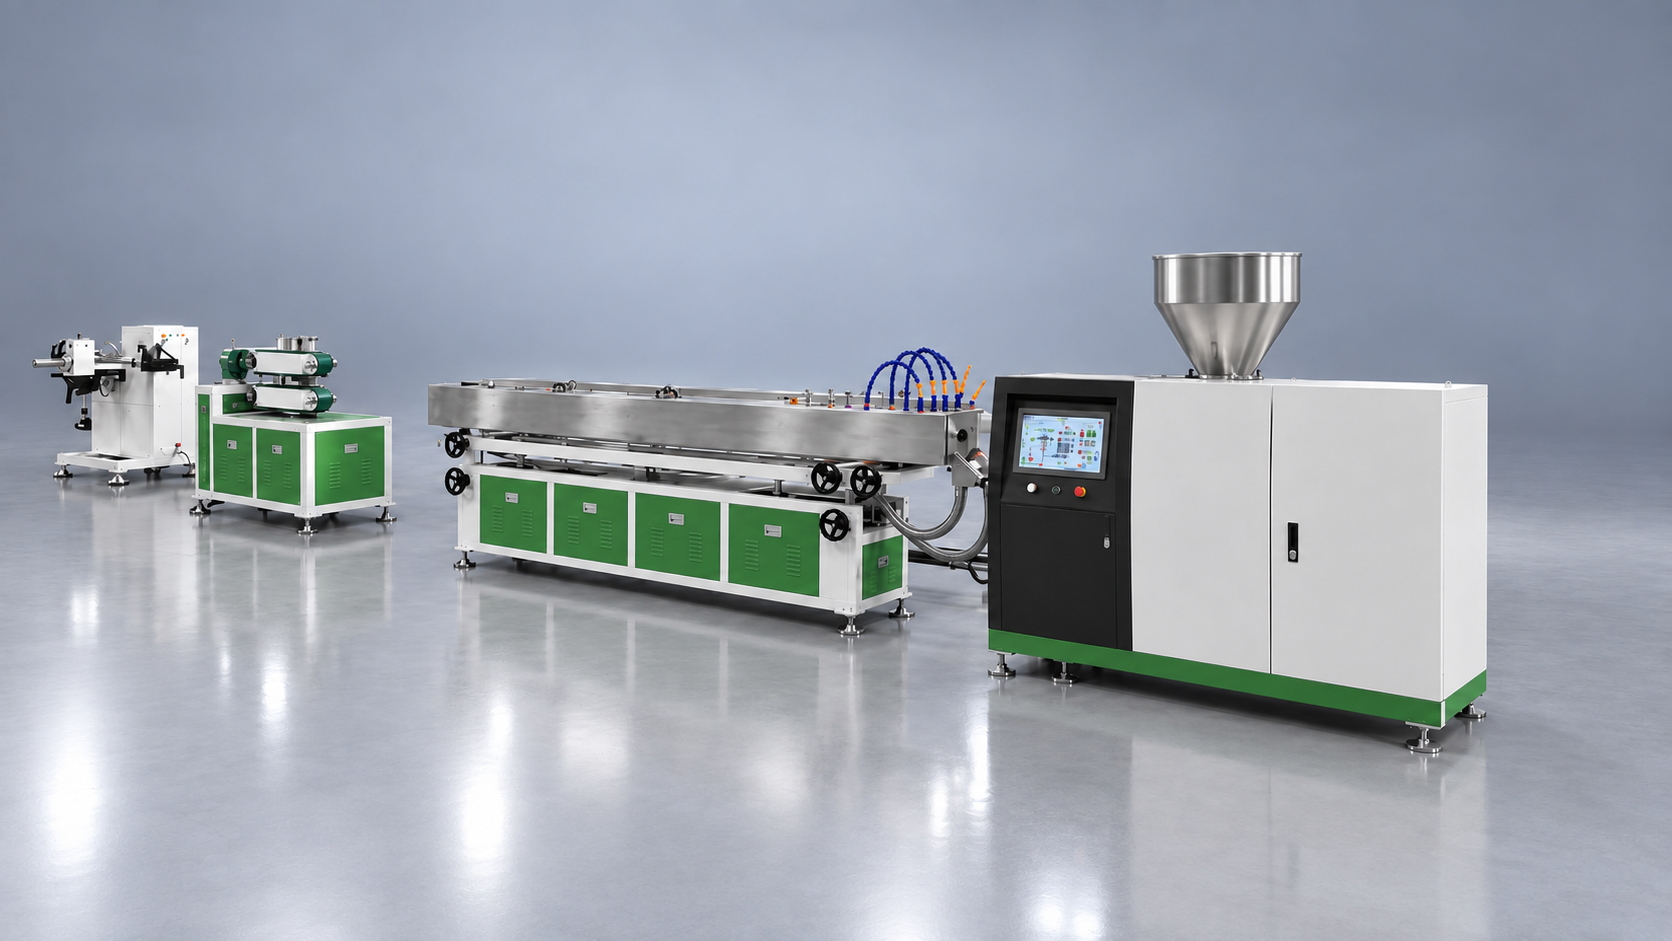
Ready to Upgrade Your Production Line?
Contact us today for a free consultation and a tailored solution.